
INTRODUCTION
The requirement for pipeline condition assessment is defined in Polish law in the Regulation of the Minister of Climate and Environment of July 24, 2023, on the technical conditions to be met by liquid fuel depots and stations, liquefied gas depots and stations, long-distance transmission pipelines used for the transport of crude oil and petroleum products, and their location [1]. This regulation requires the following inspection intervals for pipelines:
Furthermore, diagnostics prevent failures in the pipeline transmission system, which can threaten the life and health of residents, as well as the natural environment, surface water, and groundwater used to meet public needs. Due to the extensive length of transmission pipelines, often reaching hundreds or thousands of kilometers, specialized diagnostic methods are required. This necessitates the use of specialized diagnostic methods that provide information on the technical condition of the entire pipeline within an acceptable timeframe and with minimal disruption to transmission. In the diagnosis of long-distance transmission pipelines, the so-called PIG ILI intelligent pigs are primarily used [2–5]. Currently, a wide range of Pipeline Inspection Gauge In-Line Inspection (PIG ILI) intelligent pigs are available, used to detect various types of defects occurring in long-distance transmission pipelines during their operation. The most commonly used PIG ILI pigs include: − determining shape deformation; − detecting corrosion defects in the pipeline wall; − ultrasonic with a standard probe; − ultrasonic with an angled probe for detecting cracks in the pipeline wall; − magnetic MFL ILI (Magnetic Flux Leakage In-Line Inspection); − detecting deviations from the circular cross-section of the pipeline.
The operating principle of PIG ILI pigs is based, in most cases, on the introduction of a high-frequency ultrasonic wave into the pipeline wall or magnetization of the pipeline wall and reading the magnetic flux leakage generated by material discontinuities or other defects occurring in longitudinal and circumferential welds. The methods indicated above can identify defects in the pipeline wall in the form of corrosion defects, cracks, thinning, and ovalization of the cross-section. They allow for obtaining qualitative and quantitative information within a certain accuracy tolerance and within the limitations of the test method. Test methods based on the use of intelligent pigs do not provide information on the stress state in the pipeline wall. Additional local loads may act on the pipeline due to its foundation in variable soil (wet or periodically flooded soils, which causes changes in the pipeline's foundation elevation) and in terrain with spatially variable topography (the pipeline adapts to this topography, causing it to bend, resulting in additional stresses). Local installation stresses may also occur, particularly when repairs or modifications are being made to the pipeline.
It should also be noted that various types of vehicles may travel over the pipeline on unpaved roads, introducing additional loads, resulting in increased stresses in the pipeline wall. These types of local stress states are also not detected in intelligent pig tests.
In recent years, a method based on the magnetic metal memory (MMM) phenomenon, called Metal Magnetic Memory Non-Contact Magnetic Diagnostics (MMM NCMD), has been introduced in the diagnostics of underground transmission pipelines [6, 7]. During this period, it was repeatedly used to assess the technical condition of structures made of ferritic alloys of various dimensions and intended uses.
In Poland, the pioneer of the MMM and MMM NCMD contact testing method was Energodiagnostyka Sp. z o.o., which conducted tests on offshore drilling platform infrastructure. It also examined the blades and shafts of gas turbines in thermal power plants [8].
In summary, the MMM and MMM NCMD methods can essentially be considered a method for qualifying a device, i.e., approving or rejecting further operation, or as a "screening" method, allowing for the identification of structural areas requiring special attention during qualification testing. It should be emphasized that the use of this qualification method requires recognition of its effectiveness, confirmed by appropriate certificates from bodies supervising the safety of technical structures. In Poland, these are the relevant regulatory authorities, including the Office of Technical Inspection [UDT], Transport Technical Inspection [TDT], and Military Technical Inspection [WDT].
The purpose of this study is to conduct a comparative analysis of the PIG ILI and MMM NCMD ultrasonic methods. This analysis will determine the advantages and disadvantages of both methods and develop recommendations for the use of MMM NCMD in the inspection of underground crude oil pipelines and their diagnostic applications.).
MMM NCMD METHOD
The MMM NCMD test method is based on the phenomenon of metal magnetic memory, which results from the magnetoplastic effect [9]. Residual magnetization disturbs the natural distribution of the Earth’s magnetic field around the pipeline. Modern measurement methods allow for the analysis of the magnetic field around pipelines with sufficient accuracy to identify sections where the Earth's magnetic field disturbances differ from the average distribution of this field within a given pipeline section, i.e., to determine the locations of local magnetic field anomalies. In the case of ferritic steel pipelines, the source of such local anomalies may be, in particular, a local stress state in the pipeline wall that differs from the rest of the pipeline. Such local anomalies are called Self-Magnetic Leakage Fields (SMLFs) and occur in stress concentration zones (SCZs) [10-11]. In the context of diagnosing the technical condition of a pipeline, SCZ can be generated by defects occurring in the pipeline wall under the action of the internal pressure of the transported medium. They can also be the result of local, additional mechanical loads, for example, due to hydrological processes. Both causes of WMPR occurrence are important in the context of analyzing the risk of permanent pipeline damage. Examples of such inconsistencies include welding defects such as voids and cracks occurring in the welds connecting pipeline components (longitudinal and transverse welds).
The essence of the magnetic metal memory test method. The concept of "magnetic metal memory" was introduced in [6]. Previously, the terms "earth magnetic memory" were known in archaeological research, "magnetic memory" in phonography, and "mold memory effect" defined as oriented internal stresses in metal products. The concept of "magnetic metal memory" applies to ferromagnetic metals and is based on the effects of magnetoelasticity, in particular the dependence of the orientation of magnetic domains on applied loads and/or forced deformations [6]. When testing ferritic steel products, the metal magnetic memory (MPM) method utilizes magnetic effects occurring in zones of magnetic domain rearrangement, which are caused by specific mechanical loads acting on the material in these zones. It should be emphasized that when using this method to diagnose large ferritic steel objects, the primary goal is usually to detect zones with different magnetic properties. Determining the physical causes of a given magnetic anomaly requires additional diagnostic tests.
A significant feature of MPM is that it relies on magnetization by the Earth's magnetic field. This field is relatively low in intensity, especially below the ground surface, which does not inherently deform the magnetic state of the pipelines being tested. At the same time, anomalies in the magnetic state "deform" the Earth's magnetic field, allowing for the identification of pipeline sections with different magnetic states. Importantly, the Earth's magnetic field changes only slightly over distances of tens of meters. Therefore, local anomalies in this field are caused by the specific state of a given pipeline section relative to its other fragments. Considering the relationship between the magnetic state of ferritic steel pipelines and the stresses occurring, this provides a comparative basis for determining the location of sections with a specific, different stress state.
The use of MMM to assess the service life and durability of various metal structures is of long-term importance, as it seamlessly combines the capabilities of non-destructive testing, materials science, and fracture mechanics. An example of MMM use is research conducted by Energodiagnostyka Sp. z o.o., which performs a wide range of non-destructive testing on industrial infrastructure in Poland and abroad [8]. This company pioneered the introduction of MMM and MMM NCMD testing to the Polish market. Industrial research has determined that the magnetic memory of metals in new ferromagnetic products for the engineering industry reflects the characteristics of their manufacturing technology and possible manufacturing/assembly errors. Examples of products tested using MMM include turbine blades, pipelines for steam, gas, crude oil and fuels, and petrochemical products, as well as combined heat and power plants and offshore drilling platforms. The use of MMM for testing transmission pipelines is discussed in [7]. This paper describes the results of tests on underground pipelines that were shallowed above ground level due to changing thermal conditions at the pipeline's installation site, resulting from temperature fluctuations throughout the year in the permafrost areas of northern Russia. The pipelines were laid at very low temperatures, covered by a thin layer of soil. Several decades after their installation, the thermal conditions in these areas had changed by several dozen degrees, which, due to the lack of thermal compensation on the laid pipeline, caused it to deform and rise above the ground. MMM testing was facilitated in this case by the fact that the pipeline was above ground level, requiring only the removal of the anti-corrosion insulation.
This paper presents the use of MMM as a method for detecting the presence of WMPR in SCZS zones on the pipeline surface. A significant difference from the research presented in article [7] is that the MMM studies conducted by the authors were conducted after previous MMM NCMD studies of an underground transmission pipeline buried at a depth of approximately 1.5 m. It was determined that there was a disturbance in the earth's magnetic field at this location, indicating inconsistencies in the buried pipeline in this area. This represents a significant difference in the research approach.
General principles of using the MMM NCMD method. The non-contact method is based on the study and analysis of distortions in the earth's magnetic field caused by locally occurring magnetization of the pipeline due to local stresses that differ from those in other sections. Areas of the pipeline where changes in the parameters determined in the study occur are called Stress Concentration Zones (SCZs).
Local anomalies can also be the result of geometric inconsistencies in the thickness and shape of the pipes, resulting from corrosion, mechanical damage, material inhomogeneity, or cracks. Causes of SCZS include factors that act on the pipeline at a given location beyond the load resulting from the internal pressure exerted on the entire pipeline. Locally, in addition to pressure stresses, stresses generated by pipeline movement in the ground (e.g., ground movements or loads caused by vehicle traffic over the pipeline) may also occur [12]. SCZs can also be caused by assembly stresses resulting from joining pipeline pipes using welded joints and joining sheets during the pipe manufacturing process.
Strain Concentration Zones are fundamental for analyzing potential locations for crack initiation and development, and for pipeline damage in general. This stems from the fact that local stress levels directly affect the strength of a given section of a transmission pipeline. Pipeline strength, in terms of diagnosing its technical condition, should be considered in the context of crack resistance. Considering the operational conditions of pipelines, special attention must be paid to fatigue cracking. This is due to the maximum internal pressure values generating circumferential stresses in the pipeline wall, which do not exceed the design stress values, taking into account safety factors. It should also be noted that pipelines are operated at a relatively constant positive temperature, and the material from which they are made exhibits a large margin of strain hardening. On the other hand, the pressure inside the pipeline is subject to cyclical changes due to the nature of the pumping patterns. The nature of pressure changes in the pipeline over a one-year period, based on data from [12], is presented in Fig. 1.
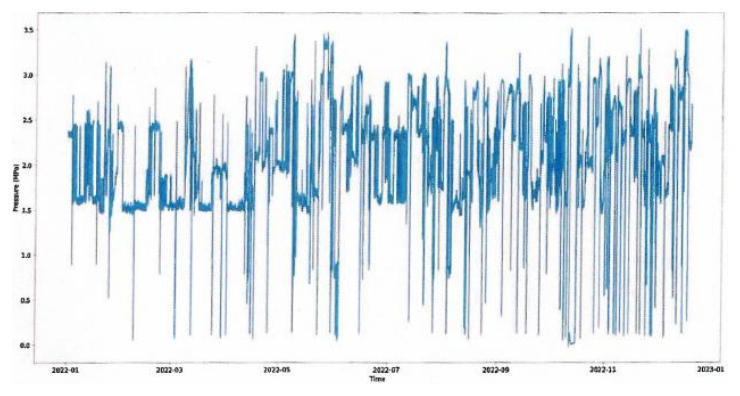
Fig. 1. Pressure changes in the pipeline over the course of one year [12]. The ordinate is the pressure value, varying in the range up to 3.5 MPa, plotted against time of measurement
As can be noted from an example of changes over one year shown in Fig. 1, there are frequent pressure drops from 2.5 - 3.0 to 0 MPa. In fact, there were over 100 such drops in the period of 2022 year. Given that underground transmission pipelines have been in operation for over 60 years, fatigue cracks are expected to pose the greatest threat to their safe operation. Fatigue cracks initially develop relatively slowly. Therefore, their presence can be detected before perforation occurs in the pipeline wall. This is accomplished by recording the local increase in residual magnetism occurring in the SCZs, resulting from changes in stress associated with changes in the strain-stress state.
TAKING MEASUREMENTS
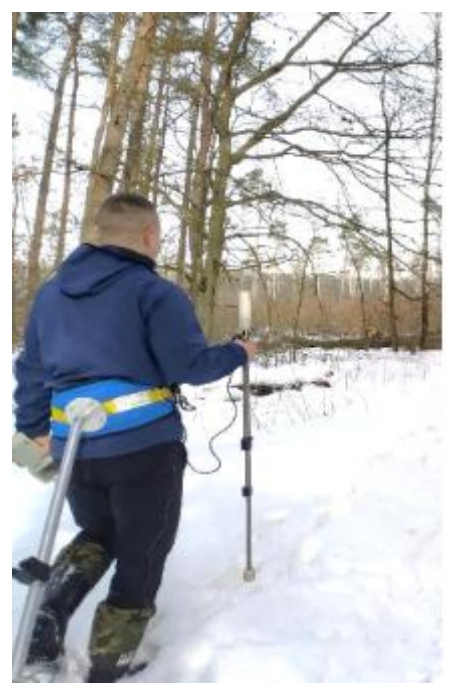
An operator equipped with a magnetic field probe (SMLF sensor) traverses the pipeline route, as shown in Fig 2.
An example measurement section with marked discrepancies determined in the PIG ILI piston tests and anomalies of the Earth’s magnetic field in the MMM NCMD tests is shown in Fig. 3.
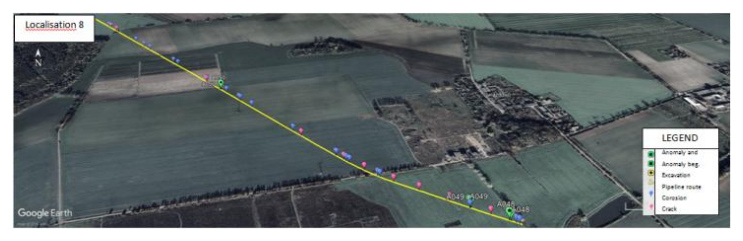
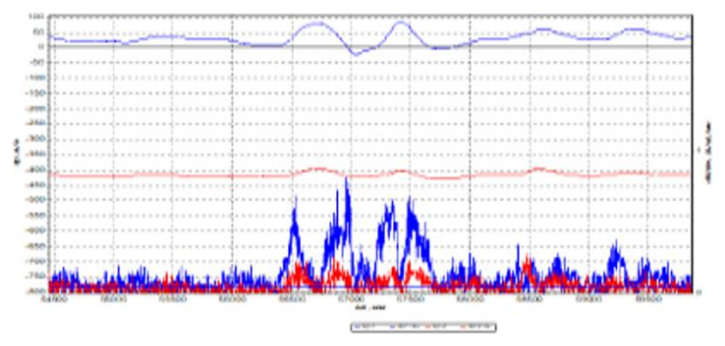
Fig. 4. Sample magnetogram from the test run. The ordinate on the left is the tangential component Hx and the normal component Hy of the magnetic field strength [A/m]. The ordinate on the right is the gradient dHx/dx, dHy/dx [A/m/mm]
Figure 4, which is provided for illustration of magnetogram shows, that as as function of probe position determined in mm, there are distinct sections with well defined magnetic disturbances. Data corresponding to the tangential component is highlighted in blue, and data corresponding to the normal component of the magnetic field strength is highlighted in red.
The essence of the MMM NCMD test is to measure the disturbances in the Earth's magnetic field components resulting from anomalies in the pipeline causing the magnetoplastic effect (Fig. 5).
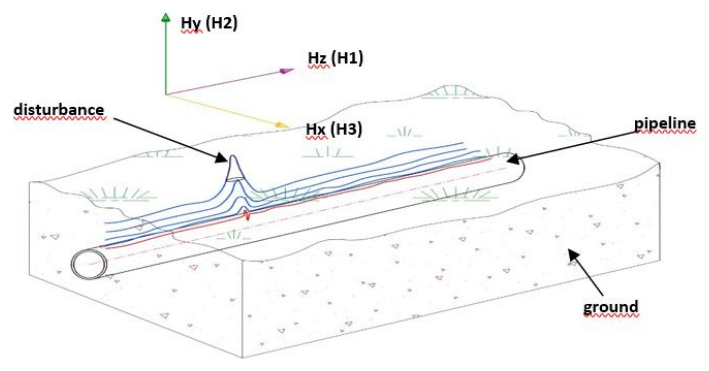
Fig. 5. Sample Schematic diagram of the disturbance of the Earth's magnetic field components [Hx, Hy, Hz] resulting from stresses, inconsistencies, and corrosion defects in the pipeline, causing a magnetomechanical effect
Therefore, measurement using the MMM NCMD method allows for scanning disturbances in the Earth's magnetic field and locating them along the pipeline route.
COMPARATIVE ANALYSIS OF RESEARCH METHODS
Underground pipeline inspections are typically conducted using inline inspection tools (ILI tools) so-called PIG ILI, with the types of these pigs being presented in Chapter 1. Intelligent pigs used for pipeline inspections, they primarily utilize ultrasonic heads, which inject ultrasonic waves into the pipeline wall at various angles. This allows for information about cracks, corrosion, delamination, and other irregularities.
In pigs that examine shape deformation, angular position sensors are used. This provides information about geometric cross-sectional deformations, dents, bulges, nozzles, gate valves, etc. MFL pigs monitor the magnetic flux leakage (the pipeline's own magnetic stray field) from the pipeline wall, indicating corrosion, defects, delamination, and cracks. Depending on the medium being transported through the underground pipeline, various types of intelligent pigs are used to examine its technical condition. Special sender-receiver chambers are required to insert the intelligent pig into the pipeline, which are an essential element of long-distance transmission pipelines.
A comparison of the MMM NCMD and PIG ILI UT methods used to test long-distance underground transmission pipelines is presented in Table 1.
Tab. 1. Comparison of MPM NCMD research methods with PIG ILI UT
The data presented in Table 1 indicate the following advantages of using the MMM NCMD method:
the ability to test pipelines not adapted for the introduction of intelligent pigs launcher and receiver facilities),
relatively high testing speed (4-8 km/day),
no need to empty the pipeline or interfere with the medium's flow,
precise location of detected anomalies (GPS accuracy +/- 10 cm),
the ability to verify the pipeline route. This is important due to the precise measurements taken with a GPS device with each measurement, which allows for the precise identification oSCZS locations,
it is relatively simple to monitor the development of anomalies through cyclical repeat testing,
detection of stress states occurring before crack development, which intelligent pigs cannot detect.
In industrial practice, limitations of the MMM NCMD method can also be identified. Tests using this method cannot be performed when the pipeline is encased in steel elements (reinforced ducts, casing pipes, reinforcing elements, etc.). Possible interference from steel elements located within the pipeline under test should also be taken into account. These elements distort the useful signal from a foreign body, giving a false impression of the pipeline's condition.
The MMM NCMD method is difficult or impossible:
in areas covered with vegetation and crops due to the need to place the sensor at a distance of 200-300 mm from the ground surface, precisely aligned with the pipeline being tested, at a constant speed (1-2 km/h). Tests are conducted
from late autumn to early spring in cultivated areas.
when conducted in difficult-to-access terrain, such as swamps, wide water obstacles, etc.
in the case of deeply buried pipelines (less than 4 m).
EXPERIMANTAL RESEARCH
This study presents a case analysis of MMM NCMD inspection of an underground transmission pipeline, conducted to prove the thesis. The tests covered a section of the pipeline on which a complete set of tests was performed using PIG ILI UT intelligent pigs and the MMM NCMD method.
The tested pipeline had a diameter of 820 mm with a wall thickness of 11 mm. It was made of St 52-3 grade steel with a yield strength of Re0.2 > 355 MPa, a tensile strength of Rm 490 - 630 MPa, and a relative elongation ɛ of up to 22%. The pipeline had been in operation for approximately 60 years and was subjected to operational loading conditions, including pressures induced by periodic agricultural operations (the nature of the loads from the transported medium in the short term is shown in Fig. 1). The tested pipeline section was located in areas with the following geological characteristics: fluvioglacial sands and boulder clays. Younger sediments are mainly boulder clays, but also include terminal moraine deposits, kame sands and silts, and fluvioglacial sands and gravels. The youngest sediments represent river sands, floodplain terraces, and lacustrine sands, silts, and clays.The pipeline section in question was tested using intelligent pigs and MMM NCMD.
The pipeline section tested by MMM NCMD and PIG ILI, with the anomalies identified for each test method, is shown in Fig. 6.
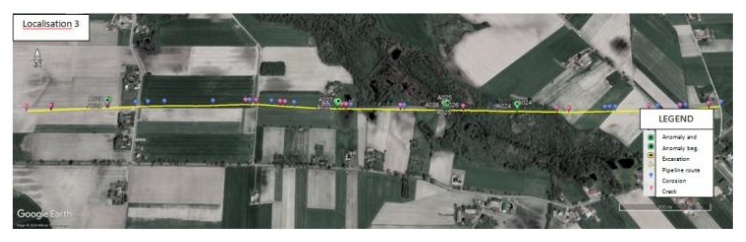
Based on the results obtained using both methods, a section was selected for detailed contact testing. The selected section showed no indications in the tests performed with the PIG ILI ultrasonic intelligent pigs, but did show indications in the MPM NCMD tests. This is shown in Fig. 7.
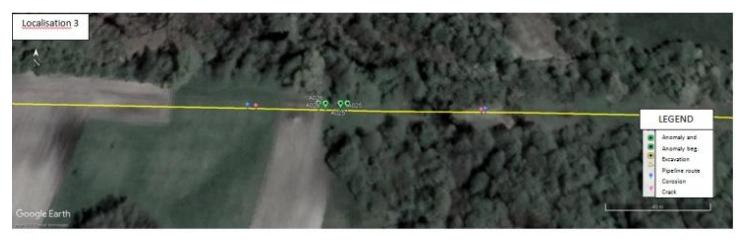
The magnetogram of the location indicated in Fig 7, selected for detailed contact MPM studies, is shown in Fig. 8. It contains data on the three components Hx (blue), Hy (red), Hz (green) of the magnetic field strength and their gradients dHx/dx, dHy/dx, dHz/dx marked with colors corresponding to the individual components.
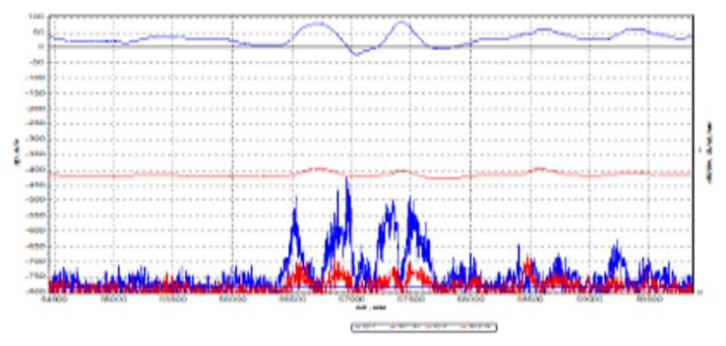
Fig.8. Magnetogram of the location indicated in photo 3, selected for detailed contact MPM studies. Ordinate on the left: Hx, Hy, Hz component of the magnetic field strength [A/m]. Ordinate on the right: gradient of the magnetic field strength dHx/dx, dHy/dx, dHz/dx [A/m/mm]. Abscissa, measuring length [mm]. Note that the plot is provided only to illustrate well defined peaks in some positions. Exact values of H and dH/dx are not analyzed
To verify the assumptions made in the conducted tests, a full pipeline diagnostic was performed at the selected locations using direct contact methods. For this purpose, after excavating the pipeline and removing the anti-corrosion coating, the pipeline surface selected for testing was sandblasted. Next, detailed NDT tests were performed, including: MMM with the probe in contact with the pipe surface, UT TOFD (Ultrasonic Testing Time of Flight Diffraction), and UT PA (Ultrasonic Testing Phased Array).
The pipeline section where the stress concentration zones and imperfections occurring in the circumferential weld S2 and longitudinal weld S1 were located is shown in Fig. 9, Fig 10.
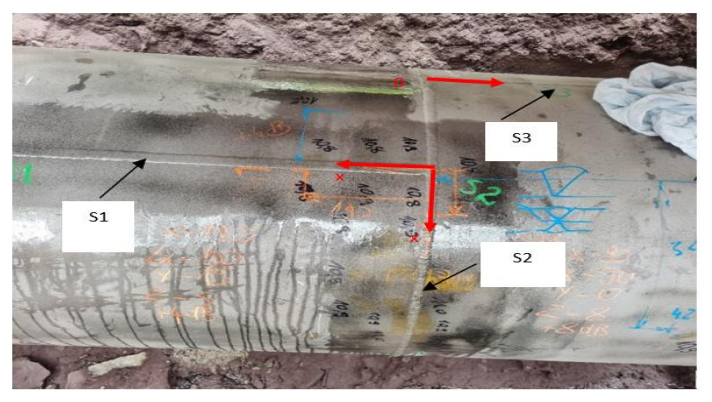
Fig. 9. A section of the underground transmission pipeline selected for detailed contact tests - MPM, UT TOFD, UT PA after MPM NCMD tests
As a result of the MMM tests, 6 stress concentration zones (SCZ) were detected, shown in Fig. 10.
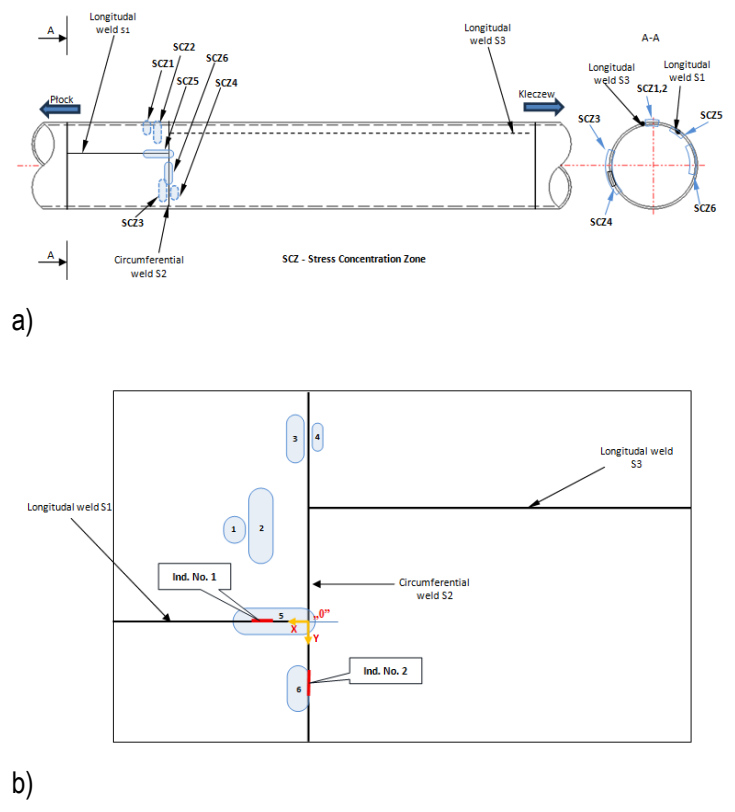
Fig. 10. Contact test results on the designated pipeline section: a) List of stress concentration zones - SCR 1 to 6 (blue), longitudinal welds S1 and S3, and circumferential weld S2; b) Development of the pipeline section showing the UTPA and UT TOFD test results plotted against the SCR determined in the MPM test. Nonconformities exceeding the acceptance levels in the UTPA and UT TOFD tests are marked in red, while longitudinal welds and the circumferential weld are marked in black
As a result of the tests using the UTPA and UT TOFD methods, it was found that non-conformities exceeding the acceptance levels occur in the SCZS 5 and 6 areas. Magnetograms for these areas are presented in Fig. 11.
As a result of the UT TOFD and UT PA ultrasonic tests of the longitudinal welds and the circumferential weld as well as the SCZS areas determined in the MMM tests, it was found that in SCZS 5 and 6, as shown in Fig. 10, defects exceeding acceptance criteria were detected in one of the longitudinal welds (S1) and the circumferential weld (S2), exceeding the acceptance levels.
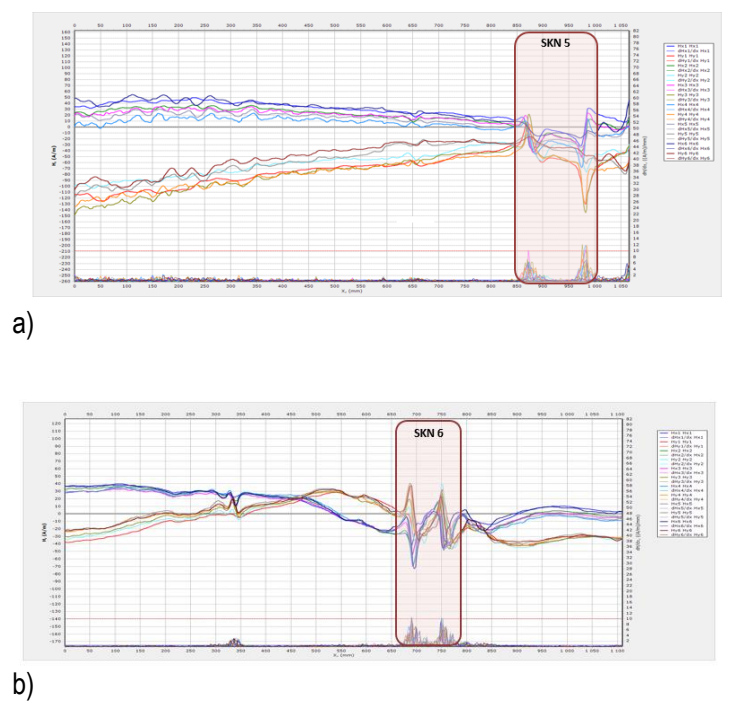
Fig. 11. Distribution of the tangential Hxi and normal Hyi components of the magnetic field strength [A/m] and their gradients dHxi/dx, dHyi/dx, i=1÷6 [A/m/mm] along the measurement length [mm]: a) SCZS 5 magnetogram; b) SCZS 6 magnetogram
Based on the contact tests, the presence of Self-Magnetic Leakage Fields (SMLF) was detected in six areas. Ultrasonic testing of these areas revealed non-conformities exceeding acceptance levels only in areas 5 and 6.
SUMMARY AND CONCLUSIONS
The results of an experimental verification of the thesis regarding the usefulness of MMM NCMD for assessing the technical condition of underground crude oil pipelines are presented. The verification was conducted through cross-field tests of one section of crude oil pipelines operating in Poland. Based on a comparison of the readings obtained during the PIG ILI intelligent pig test and the MMM NCMD method, a selected pipeline section was further examined using the contact method using advanced ultrasonic techniques: UTPA, UT TOFD, and MMM. This research program supported the thesis regarding the usefulness of MMM NCMD in assessing the technical condition of underground crude oil pipelines. At the same time, the research further clarified the general advantages and limitations of this method.
The conducted tests confirmed that MMM NCMD is a method that allows for the identification of specific stress zones in the pipeline wall, which are significantly greater than the stresses caused by internal pressure. Due to the nature of cracking processes, cracks can nucleate and develop in these areas, particularly fatigue cracks associated with cyclic changes in internal pressure from the transported medium. Therefore, areas with Stress Concentration Zones (SCZs) should be subject to special monitoring in operational inspection programs.
The conducted research has shown that at this stage of development of the MMM NCMD testing method, it is not possible to simultaneously determine the critical values of magnetic anomaly indications in relation to critical stress values. To verify the indications, it is also advisable to conduct pipeline excavations and tests using other contact NDT (Non-Destructive Testing) methods. This would clarify the nature of the nonconformity/defect.
Based on the results of NDT tests performed using various methods, a decision is made regarding the further treatment of the operating pipeline (repair, replacement of the pipeline section).
The presented research results demonstrate that non-contact magnetic field diagnostics (MPM NCMD) allows for the qualitative identification of areas with anomalies in the pipeline wall and the localization of areas with abnormal stresses, which is a significant complement to tests performed with PIG ILI intelligent pigs.
Both methods provide complementary information about the technical condition of the pipeline, with the MMM NCMD method identifying areas of specific stress in the pipeline wall, which is crucial for determining which of the indications obtained during pig tests should be given the greatest weight.
Although MMM NCMD tests are qualitative in nature, they significantly complement the results of ultrasonic tests with PIG ILI intelligent pigs. It should be emphasized that ultrasonic intelligent pigs may have limited capability in detecting certain defects in transverse and circumferential welds. They also do not detect discontinuities in the pipeline wall material located at excessive angles to the ultrasonic probes (angles exceeding 15–20° relative to the pipeline longitudinal axis). The MMM NCMD method also detects elevated stress levels in the pipeline wall caused by specific ground loads (rock mass movements, variable hydrological conditions). These stress levels cannot be detected by ultrasonic intelligent pigs currently used in the industry.
In summary, the MMM NCMD testing method is an important element in the development of underground transmission pipeline diagnostics and can be used as a complementary or screening method.
In the pipeline diagnostics process, it is advisable to create a database of test results obtained using the MMM NCMD method, PIG ILI intelligent pigs, and NDT contact tests performed in open pits. Developing such a database allows for a closer understanding of the pipeline's technical condition to its actual condition.
In short, the conducted study confirms that MMM- NCMD is an effective complementary diagnostic method for assessing the condition of underground crude oil transmission pipelines. The method enables identification of stress concentration zones that are not detectable using ultrasonic ILI tools and may represent locations of crack initiation, particularly under cyclic loading conditions.
However, MMM- NCMD remains a qualitative method and does not allow direct quantification of defect parameters. Therefore, verification using contact NDT methods is required. The integration of MMM- NCMD and ILI inspection results significantly improves the reliability of pipeline condition assessment.
It is recommended that MMM- NCMD be applied as a screening tool to identify critical areas, followed by detailed inspection using advanced ultrasonic techniques. The development of integrated diagnostic databases combining MMM- NCMD, ILI, and conventional NDT results is essential for accurate evaluation of pipeline integrity.

