
INTRODUCTION
Nickel-based alloys (often called Ni-based superalloys) are trending in both research and industry because they perform exceptionally well in extreme environments. Nickel-based alloys are high-performance materials designed for extreme environments, offering superior protection against corrosion, oxidation, and, often, high-temperature creep [1]. These properties make them essential for several rapidly growing technologies. Primarily alloyed with elements like chromium, molybdenum, and iron, they are critical in industries such as aerospace (jet engines, rocket engines, and exhaust systems), power generation (gas turbines, nuclear reactors, and heat exchangers), and processing (Chemical processing, oil and gas extraction, and pollution control equipment) [1,2]. Fe-Ni alloys like Invar 36 as well as nickel-based superalloys are considered to be hard-to-cut materials due to their high hardness, work-hardening nature, adhesiveness, and comparatively lower thermal conductivity that contribute to heat accumulation in the machining region [3]. The consequence of the mentioned properties is an increase in cutting temperature, cutting forces, tool wear rate, and deterioration of machining process performance [4]. It was found that adhesion, abrasion, diffusion, and coating degradation were the main wear modes occurring during machining, whereas the effect of cutting speed and feed rate on tool wear rate and surface quality was considerable [5]. Besides, the thermal and mechanical loads developed during machining process cause the increase in force fluctuations and dynamic instability leading to vibration intensification and faster tool wear [6]. Invar, also known as Invar 36 or FeNi36 (roughly 64% iron, 36% nickel), is recognised for its uniquely low thermal expansion. This makes it an attractive option for manufacturers in applications where the temperature variations are extreme [7-10]. Invar 36, although very effective and widely in demand, presents difficulties during machining. Invar 36 is considered difficult to machine because it is ductile and has low thermal conductivity, leading to rapid tool wear, stringy chips, and high heat buildup [11].
Process variables such as speed, feed, and cutting depth are crucial and significantly influence material removal rate and surface finish in machining operations [12]. Conventional machining is an important operation where machining takes place at room temperature without the use of any coolant or cutting fluids. It has many economic and environmental advantages as it helps in reducing machining costs and hence the environmental effects related to the disposal of cutting fluids [13]. In machining operations, the roughness attained on the surfaces has significant effects on the efficiency of the machined components and the quality of the product. Machining parameters, along with tool-related parameters comprising tool wear and tool geometry, have major effects on the obtained surface roughness [14]. Surface roughness may also be significantly impacted by characteristics of the work material, such as hardness and grain size [15]. Some research has indicated that decreased roughness also enhances the corrosion resistance, thus requiring a finer surface to maximise the protective effect against the corrosion [16].
In machining operations, the wear mechanism is an important factor since it directly affects tool life, efficiency of machining, and the obtained surface quality of the component. Tool wear may occur by different mechanisms such as abrasion, adhesion, chemical, thermal, or mechanical phenomena [17]. Also, the relationship assessment between tool behaviour and the vibration during machining operation is a critical area of research. Vibration of higher magnitude may lead to a reduction in machined performance, increased tool wear, and poorer surface quality of the component. In this regard, tool wear has often been assessed through statistical measures in terms of Root Mean Square (RMS) values of the vibration signals [18]. Experimental studies have indeed validated the vibration signal as a method of monitoring tool wear, showing a good relationship between the development of tool wear and the characteristics of vibration [19,20].
A full factorial design is an extensive experimental procedure for studying the effects brought about by multiple factors on machining performance. It involves conducting experiments for all possible combinations of factor levels. It provides the possibility of a thorough study of the interactions between machining factors [21]. The multi-criteria decision-making techniques, also known as Multi-criteria decision-making (MCDM) techniques, are highly effective in solving complex optimization problems in machining because of their capability to accommodate different inconsistent criteria. This attribute is extremely useful in machining studies, where the optimization of process variables is a must in order to attain the required results, including reduced surface roughness, minimum tool wear, and machining vibration, etc. [22]. The complexity in relationships among the variables can be solved through MCDM techniques such as Grey Relational Analysis (GRA), Distance from Average Solution (EDAS), and Additive Ratio Assessment (ARAS) [23].
Current studies on machining Invar 36 are very limited. Zang et al. [24] investigated the chip formation and chip-flow behavior during the machining of Invar36. Orthogonal cutting experiments were performed, mechanical properties and deformation behavior were measured, and the chip morphology and microstructure were analyzed. A flow stress constitutive model was developed based on material tests, a polycrystalline finite element modelling was used to simulate chip formation, and the stress distribution and deformation patterns were analyzed during cutting. It was noted that, increasing cutting speed leads to higher plastic deformation rates, increased shear localization, and more frequent and pronounced serrated chips. Khanna et al. [25] employed Taguchi's methodology to machine INVAR 36 alloy using the end milling process. Optimizing the process variables to achieve minimum roughness was the objective of the study. They found the cutting depth as the major influencing factor affecting the roughness of the alloy, followed by speed and feed, respectively. Based on the identification of specific optimal parameters, they were able to achieve an optimal quality surface with a low surface roughness value of 0.1835 µm. Mahir et al. [26] investigated the machinability of Invar36 during turning using three types of carbide cutting inserts, namely Uncoated carbide inserts, AlTiN coated carbide insert (single-layer coating), TiCN–Al₂O₃ coated carbide insert (multi-layer coating). Machining was conducted to evaluate tool performance based on four main responses, such as cutting force, surface roughness, tool flank wear, and power consumption. The multilayer coated insert performed the best among the three tools. Tool wear reduced by up to 30% compared with single-layer coated insert, up to 60% compared with uncoated insert. The multilayer coated insert also produced the lowest surface roughness. Uncoated inserts showed higher roughness due to rapid tool wear and adhesion effects.
Jovicic et al. [27] investigated dry turning of Inconel 601, which is known for poor machinability. The objective of the study was to model the machining process, optimize machining parameters, and achieve a balance between roughness, flank wear, MRR using optimization approach. It was observed that increasing the feed and speed increased the value of MRR, but increasing the feed adversely affected roughness and flank wear. Feed had one of the strongest influences on all three outputs of the study. Overall, they proposed a hybrid ANN–GA optimization framework, showing that proper control of feed, speed, and tool geometry can simultaneously improve surface finish, tool life, and productivity with prediction errors below 2%. D'Mello et al. [28] performed an experimental work to analyze the effect of cutting vibrations on roughness in high-speed turning of Ti-6Al-4V. Remarkably, they observed that with increased tool wear, the surface quality improved. Feed had a significant effect on roughness responses Ra and Rt, explaining more than 70% variation in results. Rao et al. [29] aimed to optimize turning parameters during machining of Inconel 718. They tried to simultaneously improve multiple responses such as roughness, tool wear, MRR using two MCDM techniques namely, GRA and Technique for Order of Preference by Similarity to Ideal Solution (TOPSIS). Both GRA and TOPSIS successfully optimized turning parameters. The two methods produced different optimal parameter combinations. GRA provided an optimal condition for better improvement in surface roughness and tool wear. Whereas the TOPSIS provided a condition that resulted in a higher material removal rate.
Eskandari et al. [30] conducted a study to optimise machining parameters during the turning of N-155 alloy. The main goal was to simultaneously optimise multiple machining responses using GRA combined with the Taguchi method. The optimal parameter combination identified using GRA provided good results. Abbed et al. [31] conducted a study to investigate the effect of tool materials and process variables on the turning performance of titanium alloy. The goal of the study was to model and optimize machining conditions using statistical analysis and several MCDM methods such as CoCoSo, MABAC, ARAS, and CODAS. Feed rate strongly affected surface roughness. Speed and cutting depth significantly influenced cutting forces. Tool material also had a noticeable effect on machining performance. The ranking results from CoCoSo, MABAC, ARAS, and CODAS were largely consistent, which confirmed the reliability of MCDM approaches for machining optimization. Sivalingam et al. [32] investigated the machining of Inconel 718 during the turning process. The main goals of the study were to improve surface quality, increase tool life, and identify optimal machining parameters. To achieve this, they applied MCDM techniques such as ARAS and CODAS. Both MCDM methods produced similar optimal solutions, validating the reliability of the optimization approach.
Although there are few relevant studies available in the current scenario related to Invar 36, there is a substantial research gap in the current literature with respect to a complete comparative study of surface roughness, tool wear, and machining vibration, and MCDM approaches, particularly in the context of turning operations with Invar 36. This work addresses the gap in the literature by providing an in-depth quantitative analysis for the dry turning of alloy Invar 36. The research adopts a full factorial experiment design with three levels, which combines the values of Ra and VBmax measured after every pass with the measured vibrational signals. The application of GRA, EDAS, and ARAS offers an overall optimization strategy that can be applied for evaluating the impact of multiple machining responses during the dry turning of Invar 36. Therefore, the objective of this research is to conduct experiments on the influence of cutting speed (vc), feed rate (vf), and depth of cut (ap) on surface roughness (Ra), VBmax (maximum flank wear) and machining vibration (RMS) when dry turning of Invar 36 in the case of high-speed machining process. Furthermore, FFT-based frequency domain analysis is used for exploring the dynamics of the machining process and giving mechanistic interpretation of the relationship between tool wear, vibration, and surface roughness.
METHODOLOGY
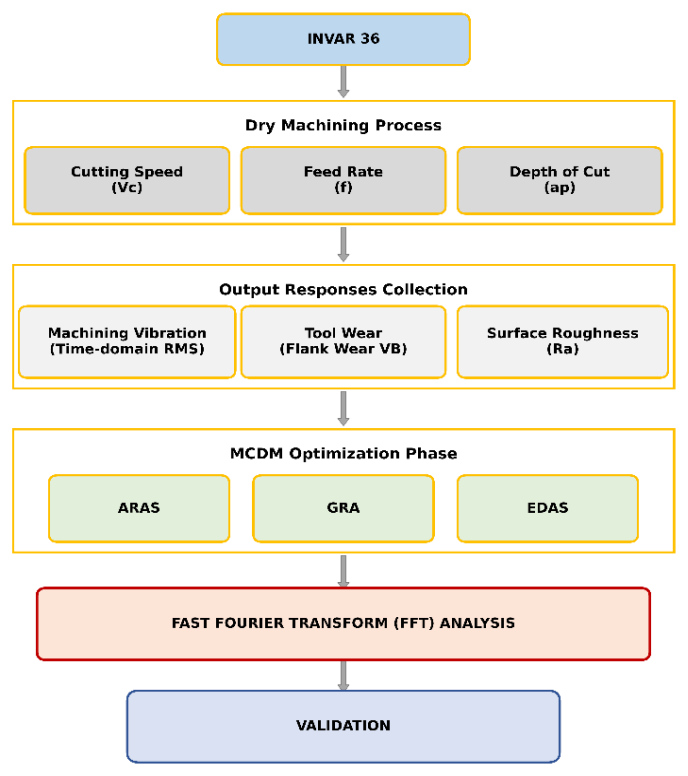
The methodology of the study has been depicted in Fig. 1.
Experiments
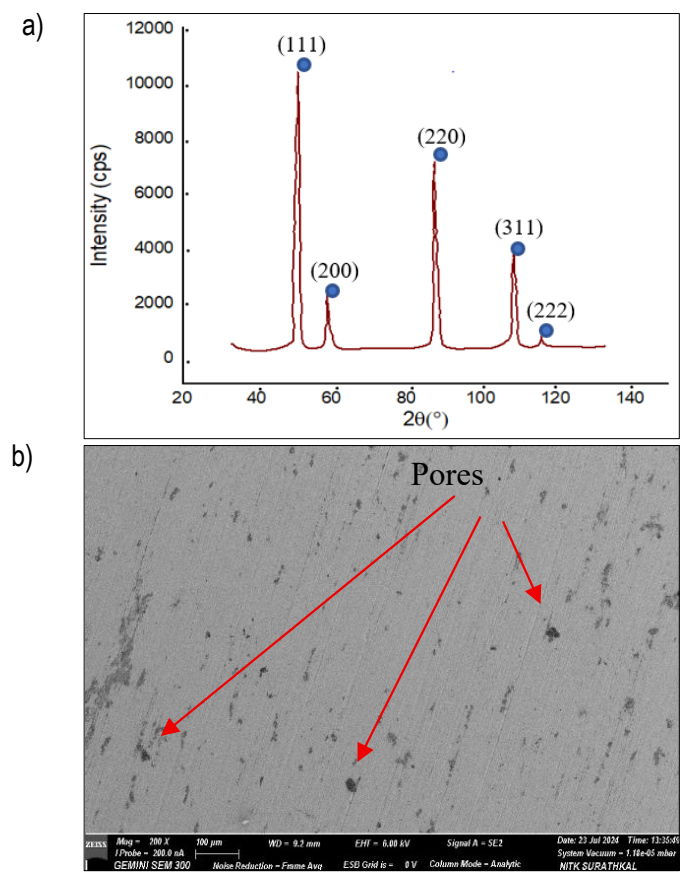
The alloy was received as a cylindrical rod measuring 220 mmx50 mm. The specifics of the alloy Invar 36 are displayed in Tab. 1. Fig. 2. (a) presents the XRD pattern of the alloy, where the hkl indices are recognized as 111, 200, 220, 311, and 222, which are from the Austenitic FCC phase of the composition, identified at 52°, 60°, 89°, 111°, and 119°, respectively [33]. The microstructure of the alloy surface taken from a Scanning Electron Microscope (FESEM) (GEMINI300) is presented in Fig. 2 (b). The microhardness of the raw material (as-received) is found to be 220 HV.
The engine lathe used for this process has a maximum speed of 1,800 RPM and a 10 HP motor. The spindle speed can be accurately controlled by a 3.7 kW (5 HP) AC inverter drive equipped with a motor-operated potentiometer (MOP). Since the engine lathe allows the spindle speed to be varied in a limited number of preset values, the inverter AC drive is necessary to dynamically vary the spindle speed in RPM to the dynamically decreasing diameter of the workpiece during the machining operation. The AC inverter motor allows the dynamic variation of the cutting speed to be translated to a dynamic variation of the feed rate. This is necessary to ensure that the spindle speed is varied accurately, thus maintaining a constant MRR. The implementation of the AC inverter motor is necessary to ensure that the results of experiments are accurate and precise.
The cutting parameters for conducting the experiments have been selected using a 3-level design for the range of variables presented in Tab. 2. Turning was performed in a dry environment for all the experiments, and a single-pass experiment was carried out with a constant machining length of 60 mm. For this, the workpiece was divided into three sections, each measuring 60 mm, with each section being designated for a single machining pass. The tool and machine parameters are detailed in Tab. 2. The dry machining has been schematically represented in Fig. 3 (a), and the actual setup is presented in Fig. 3 (b).
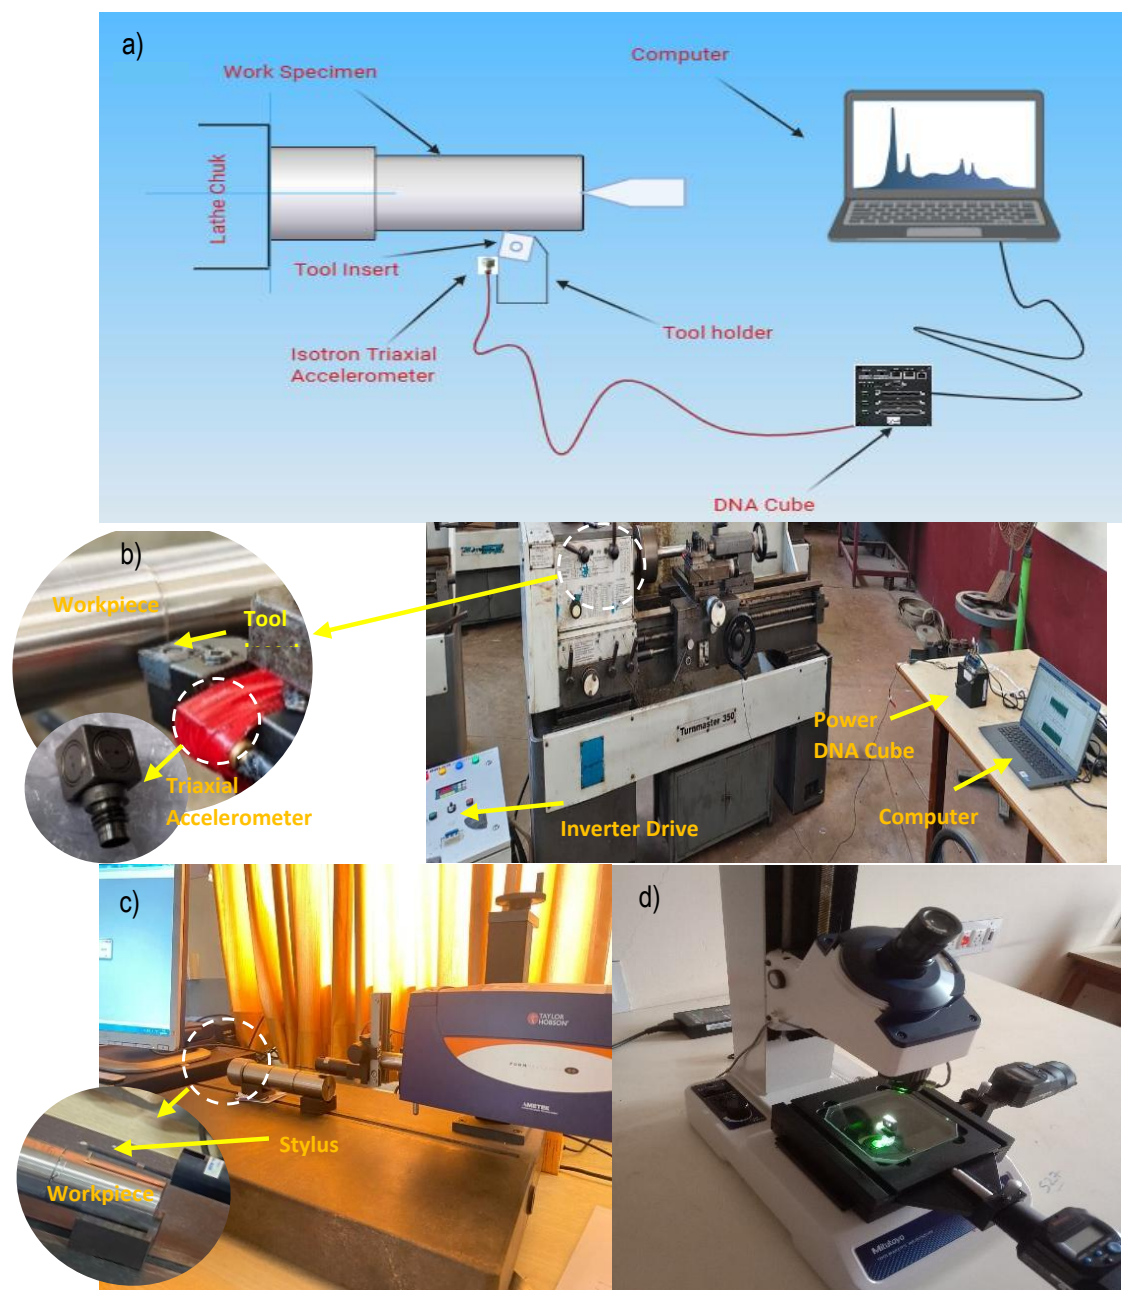
Fig. 3 (a) Schematic of the setup, (b) Actual setup, (c) Surface roughness testing, (d) Tool wear testing
Tab. 2. Machining conditions and parameters
Data regarding the key outputs, such as roughness, tool wear, and vibration, are collected. Measurements of vibration signals were carried out through a triaxial accelerometer in three perpendicular directions, which are radial (Vx), feed (Vy), and tangential (Vz). A Model 65-10 Isotron triaxial accelerometer was used to capture the signals coming from the vibrations in real time. The analog signals obtained from the experiment were transmitted to a DNA-PPCx at a high frequency of 10 kHz. The UEI Power DNA
cube ensures a smooth acquisition and conversion of data. A computer with LabVIEW software was linked to this system, which is a storage of the high-frequency data produced during the machining process. The root mean square of the obtained signals was then calculated to facilitate the reading of the intensity of the signals. RMS analysis is a fundamental analysis of the intensity of the signals, while other variables, such as the peak amplitude, show the highest point of the signals. Microsoft Excel 2016 was used for the calculations. The formula applied for the RMS calculation is:

where, n = is the total number of vibrations that are recorded in the selected steady state cutting period, xi = vibration amplitude of the ith sample.
Further, a contact-type 2-D profilometer (TalySurf 50) was used to measure the roughness of the workpiece at three different locations along the circumference, spaced 120° apart. Measurements were taken using a sample length of 2.5 mm after each machining pass (Fig. 3 (c)). Additionally, as shown in Fig. 3 (d), the flank wear of the tool was inspected using a Tool Maker's Microscope (Mitutoyo) after each machining pass. The data obtained is analysed statistically with the help of Response Table Analysis. Many researchers [34-39] focused on the impact of process variables on output responses during machining operations have utilized Response Table Analysis to identify which process variable has the most significant effects on these outcomes.
Multi-criteria decision-making (MCDM) techniques optimization
For the determination of the optimal machining process parameters taking into account RMS vibration, flank wear, and surface roughness at the same time, three well-known MCDM methods such as GRA, ARAS, and EDAS were considered. As all criteria have to be minimized in the problem, the smaller-the-better approach has been used in the analysis.
Grey Relational Analysis (GRA)
Normalizing the measured values: the smaller-the-better criterion is expressed as:
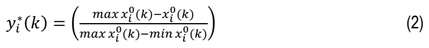
Here, xi0(k) =original value, i =tests, k =quality characteristic, and yi*(k) =value after grey relation generation.
GRC:
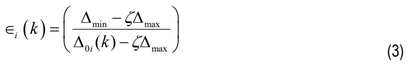
Here, ∆0i(k) =offset in the absolute values between the reference yo*(k)yi*(k) and comparability yi*(k) yi*(k)sequence, ζ =distinguishing coefficient, ∆min and ∆maxare the least and highest of ∆0i(k).
Grey Relational Grade (GRG)

Here, γi =(0 to 1), and n =experiments.
Ranking: ranking is given based on the highest GRG values.
Additive Ratio Assessment (ARAS)
Decision making matrix:
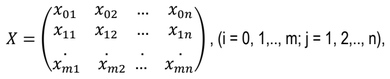
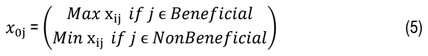
Weighted normalized decision matrix:
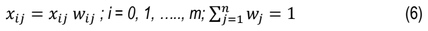
Optimality function:
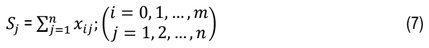
Degree of utility:

where, Si and So are the optimality criterion values.
Distance from Average Solution (EDAS):
Average solution:
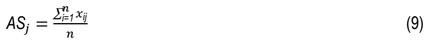
Distance from average:
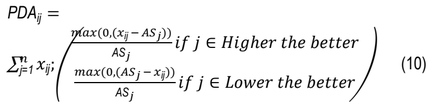
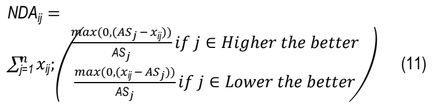
where, PDAij and NDAij denote the positive and negative distance of ith alternative from average solution in terms of jth criterion, respectively.
Appraisal score:

A higher appraisal score shows better overall performance of the machining parameters. Here, all calculations and analysis involved in the MCDM methods were implemented with the use of MS Excel 2016 software.
RESULTS AND DISCUSSION
Experimental results
1 Influence of process parameters on RMS, VBmax and Ra
The results of the machining experiments are presented in Tab. 3.
Tab. 3. Results of the experiments
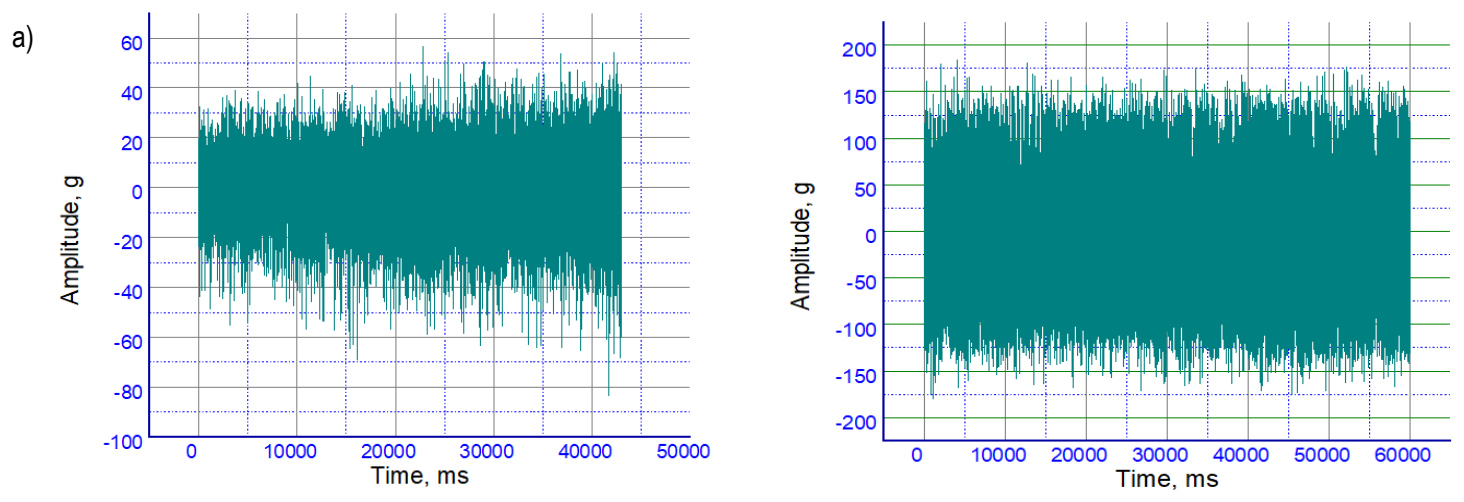
The vibration responses were recorded simultaneously along radial (Vx), axial (Vy), and tangential (Vz) directions during the dry turning process. Out of the above-mentioned vibration components, radial vibrations (Vx) play an especially significant role since this type of vibrations changes the instantaneous depth of cut, and as a consequence, the interaction of the tool and workpiece is affected. Changes in the effective depth of cut cause the changes in chip thickness, cutting forces, material separation mechanism, which are finally observed in the surface roughness. The radial vibrations have much more significant impact on surface roughness compared to the other two vibration components, axial and tangential, because radial vibration changes cutting geometry and surface generation mechanism. In addition, flank wear increases the contact length between tool and workpiece and causes force fluctuations and vibration amplification in radial direction. Thus, radial vibration is very sensitive to both the wear progression and deteriorated surface quality [40]. Vibration data analysis allows the understanding of the dynamic features of the machining process. Concentrating on time-domain signals, the researchers are able to see how machine vibrations change during machining [27]. With regard to the computation of RMS, the vibration signal was continuously collected during each of the machining trials. The RMS computations were done using the steady state cutting portion of the vibration signal recorded. The transient portions of the tool entering and exiting were not used in the computations since these portions had impact vibrations and not the actual cutting vibrations. Only the steady state cutting portion was used in computing the RMS. Time-domain signals of the vibration measured can be seen in the graphs in Fig. 4. The X-axis is time in milliseconds, and the Y-axis is acceleration amplitude in g. Figure 4 (a) shows the signal that corresponds to the minimum RMS vibration recorded, which was 14.246 g. The waveform has narrow fluctuations in amplitude of about ± 60 g. Conversely, the signal for the highest RMS vibration recorded is shown in Fig. 4 (b), captured at vc=200 m/min, vf=0.18 mm/rev, and ap=1.2 mm. The acceleration here is far higher, showing wide fluctuations exceeding +150 g. The large difference between the vibration levels in the lowest (Fig. 4 (a)) and highest (Fig. 4 (b)) conditions clearly explains the variation in vibration levels because of various experimental conditions. Stable vibration levels ensure optimal machining conditions, improving the quality and stability of the machining process [41,42].
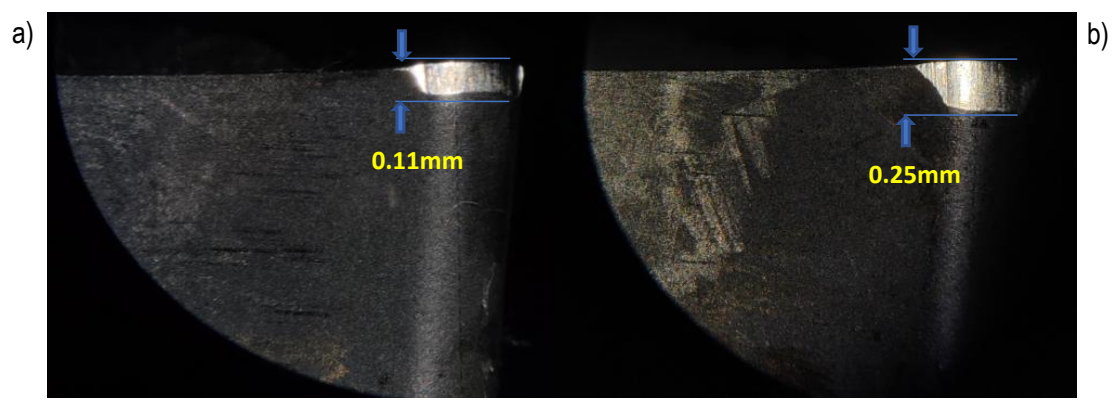
Tool wear parameter VBmax is a critical performance characteristic, with significant variation across the experiments observed in the present study. The lowest measured tool wear, 0.11 mm VBmax (Fig. 5 (a)), was obtained under the following cutting conditions: vc=150 m/min, vf=0.28 mm/rev, and ap=0.8 mm. On the other hand, the highest tool wear of 0.25 mm VBmax (Fig. 5 (b)) was observed when the process variables were vc=200 m/min, vf=0.28 mm/rev, and ap=0.8 mm.
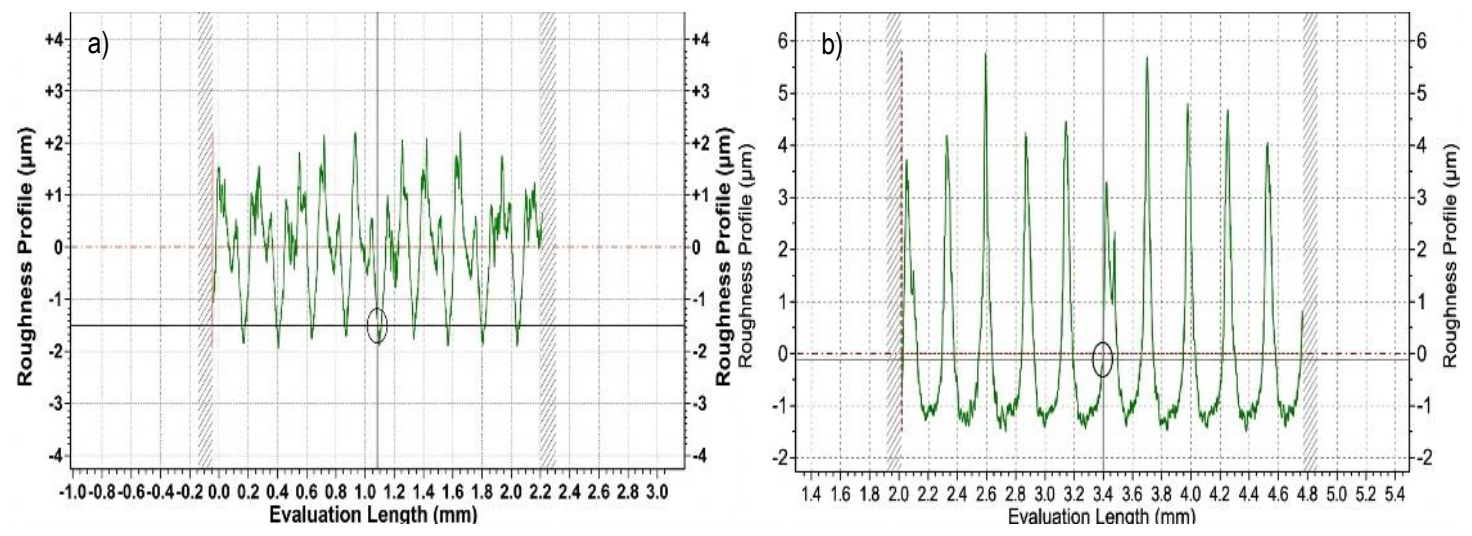
The direct impact of process variables on workpiece machined surface is demonstrated by the two different machined surface roughness profiles shown in Fig. 6. For specific conditions of vc=200 m/min, vf=0.24 mm/rev, and ap=0.8 mm, the surface having the smoothest profile is depicted in Fig. 6 (a) with the least magnitude consistent peak values. On the other hand, as shown in Fig. 6 (b), the roughest surface profile is produced at vc =150 m/min, vf =0.28 mm/rev, and ap =1.0mm, with more noticeable peaks and valleys. These two profiles (Fig. 6 (a) and (b)) are compared to emphasize the different surface finishes that are able to be achieved through machining operations. Their significance lies in drawing attention to the importance of determining specific combinations in ensuring final surface quality during machining.
Response table analysis and main effects plots
Response Table Analysis results for the effect of process variables on RMS, VBmax, and Ra are shown in Fig. 7 and Table 4. According to the analysis, cutting speed is the most influential parameter in relation to both RMS vibration and VBmax, while the feed rate parameter is the most influential in relation to Ra. In regard to RMS vibration, cutting speed had the highest Delta value since cutting speed differences caused the most significant change in vibration amplitude. During dry turning process, increasing cutting speed causes higher temperatures, frictional interaction, and dynamic load at the interface of the tool and workpiece, leading to vibrations [43]. The feed rate was the second most influential parameter because the higher the feed rate, the higher the chip load and the cutting force, leading to higher vibration values, while the depth of cut is the least influential parameter. Similarly, the greatest change (Delta value) in VBmax was recorded with increasing cutting speed. The main reason behind the significant effect of cutting speed is the high thermal and tribological loading on the cutting edge. Several researchers have found that increased cutting speeds cause the processes of adhesion, abrasion, and wear due to the high temperature levels developed during machining difficult-to-machine nickel-based alloys [44]. Moreover, the reason behind the limited thermal conductivity and adhesion properties results in low heat dissipation from the cutting area leading to flank wear formation. Increased mechanical loading of the cutting edge is another reason behind the effect of feed rate on the process of wear [41]. With regard to surface roughness, the feed rate was found to be the predominant influencing factor. Some researchers have indicated that this is in accordance with the basics of turning operations, since the feed rate determines the distance and height of the feed marks that are produced on the surface. The surface profile height increases theoretically with an increase in feed rate; thus, there is an impact on the quality of the surface finish. There is a direct influence of the vibration characteristics between the tool and work piece in determining the topography of the surface during turning operations. Hence, even though vibration affects the surface, the feed rate is the primary factor for determining the surface roughness. Depth of cut followed feed rate as it affects vibrations and cutting force [40]. The RMS (Root Mean Square) vibration value is often used in the machining process to evaluate the state of the tool due to the fact that vibration energy normally grows while the tool wears out. A comparison of Fig. 7(a) and Fig. 7(b) reveals a certain connection between RMS vibration and VBmax under the studied cutting conditions. Increased flank wear tends to result in higher vibration values, whereas lower flank wear is related to smaller vibration amplitudes [44]. Such results may be explained by the higher friction coefficient at the interface between the tool and the chip, irregularity of chip formation, reduced sharpness of the cutting edge, increased cutting forces, and dynamic instability created by the worn cutting edge. All these factors contribute to higher vibration amplitude and vibration energy, consequently increasing the RMS value [45,46].
However, it has been noted that the response of surface roughness was different from the response of tool wear. Generally speaking, the increase in tool wear results in an increase in surface roughness during the machining process. However, sometimes surface roughness decreases in spite of an increase in tool wear. As a result, a slight burnishing effect appears on the surface of the workpiece, which makes the surface better in spite of the wear that exists. Such situations were also observed during the machining of difficult materials, like titanium [28]. Hence, even though the excessive tool wear leads to a worse surface, the moderate wear can make the surface better.
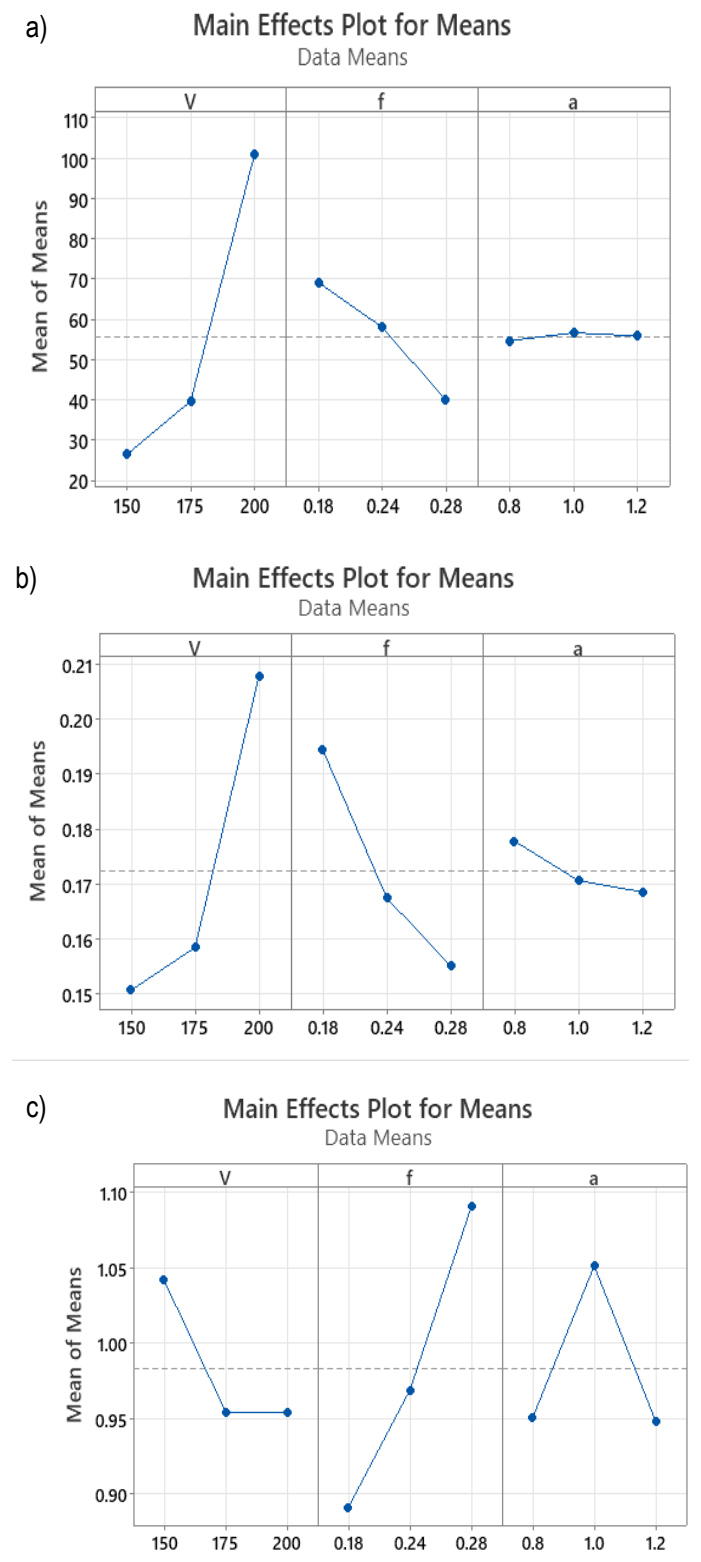
Fig. 7 Main Effects Plots- Behaviour of (a) RMS, (b) VBmax, (c) Ra with respect to process parameters
Tab 4. Response Table for RMS, VBmax, and Ra
Optimization results
Grey Relational Analysis (GRA)
Tab. 5. shows the implementation of GRA for optimizing the responses Ra, VBmax, and RMS values. First, weightage is allotted equally with the value of 0.33 for surface roughness (Ra), tool wear (VBmax), and vibration (RMS). The experimental results are normalized (normalized Ra, VBmax, RMS) in such a way that all responses vary between 0 and 1, where 1 is the optimal response for all. The Deviation Sequence is obtained by finding the deviation between the normalized response and optimal response (1), followed by calculating the Grey Relational Coefficient (GRC) for all responses. The Grey Relational Grade (GRG), or overall response measure, is an average value of GRC. ranks have been allotted based on the highest to lowest GRG values. From the GRA method, the Exp. No. 3 (vc = 150 m/min, vf = 0.18 mm/rev, ap = 1.2 mm) is ranked first with GRG value of 0.772.
Tab. 5. Results of Grey Relational Analysis (GRA)
Additive Ratio Assessment (ARAS)
Tab. 6. illustrates the results of the ARAS method applied to data obtained from the experiments. Positive and negative distances from the average solution are identified based on whether the criterion is helpful or unhelpful. Normalization is the initial step that is subjected to output responses, namely Ra, VBmax, and RMS. The resulting values are then multiplied by the weight
corresponding to the criteria to get the values under the columns of the Weighted Decision Matrix for Ra, VBmax, and RMS. These weighted values are the relative importance of each response to an experiment. Here, 0.33 is the weight assigned to each output response. Further, the method involves calculating the appraisal score and utility degree (Ki) to rank the experiments. The condition with the highest utility degree value is assigned Rank 1. The final ranking showed that the optimal experimental condition reached the highest Ki value of 0.920. This top-ranked experiment is Exp. No. 3 corresponds to vc =150 m/min, vf =0.18 mm/rev, ap =1.2 mm.
Tab. 6. Results of Additive Ratio Assessment (ARAS)
Distance from Average Solution (EDAS)
Tab. 7. illustrates the results of the EDAS method applied to data from the machining experiments. First, the average value of each criterion was calculated and treated as the reference solution. Based on this reference, the PDA and NDA values are calculated for each experimental value. These values are multiplied by respective normalised weights to obtain the weighted positive and negative distances. The summation of weighted PDA values results in the Positive Score (SP), while the summation of weighted NDA
values yields the negative score (SN). SP and SN were normalised to obtain the Normalised Positive Score (NSP) and Normalised Negative Score (NSN). The Appraisal Score Index was then calculated using the normalised scores to represent the overall performance of each experiment. The experiments were ranked based on their Appraisal Score Index (ASI) values, where a higher ASI indicates better performance. The highest ASI value of 0.968 was obtained for Exp No. 3, indicating optimal turning condition among all 27 experimental conditions. This top-ranked experimental condition corresponds to vc =150 m/min, vf =0.18 mm/rev, ap =1.2 mm.
Tab. 7. Results of Distance from Average Solution (EDAS)
The rankings calculated based on GRA, EDAS, and ARAS showed that Experiment 3 (vc = 150 m/min, vf = 0.18 mm/rev, ap = 1.2 mm) was the optimal process condition for machining operation. While Experiment 3 did not show the lowest surface roughness value, it produced the lowest vibration (RMS = 14.246 g) and lowest flank wear (VBmax = 0.110 mm) values. Considering that multi-criteria optimization looks for the best compromise solution with respect to conflicting criteria, the overall high performance of Experiment 3 gave it the top position in the ranking. From the viewpoint of the machining operation, a low cutting speed decreased the frictional heat and temperature at the tool-chip interface and slowed down wear formation and ensured cutting edge integrity. Such behaviour has been observed in machining of hard-to-cut alloys when cutting speed increases and wear formation gets faster due to the increase in thermal and tribological aspects [43-46]. A low feed rate (0.18 mm/rev) led to a decrease in the chip load and force fluctuation, ensuring dynamic stability and low vibration level. Earlier investigations have proved that low vibration amplitudes ensure higher machining stability and prevent the excessive wear of the cutting tool and machined surface [47–52]. While the minimum surface roughness was attained under varying machining conditions, Experiment 3 was found to have the lowest vibration and tool wear values at the same time. However, because multi-criteria optimization involves obtaining the optimal compromise among the performance metrics rather than obtaining the optimal value of one response alone, the combined performance of RMS vibration and VBmax overcame the slight increase in surface roughness to give Experiment 3. This is in accordance with the suggested mechanistic feedback-loop model which states that tool wear, vibration and surface quality develop in an interrelated manner and hence should not be considered in isolation [47-52].
The consistent selection of experiment 3 by GRA, EDAS and ARAS shows that the process of optimization was very successful and confirms that the stable machining conditions characterized by
low vibration and low tool wear yield the best machining performance in the case of dry turning of Invar 36.
Vibration Analysis using Fast Fourier Transform (FFT) of Machining Stability
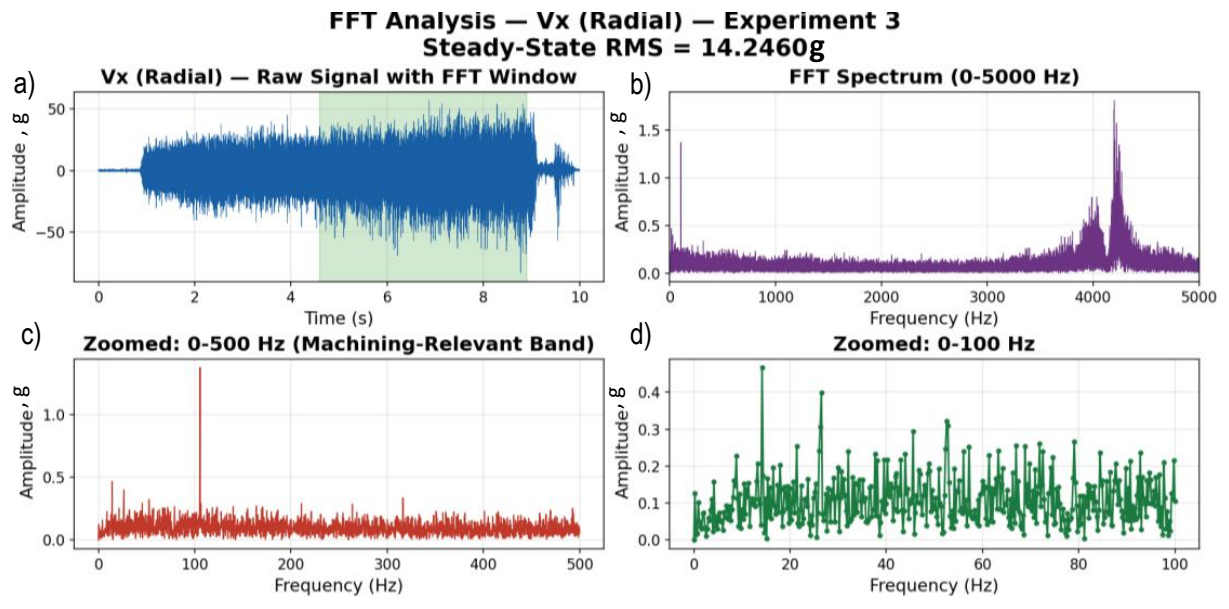
FFT Analysis – Vx Radial for Experiment 3
The Vx (radial vibration signal) obtained in Experiment 3 consists of three phases as can be seen in Fig. 8(a), a phase with low vibration level at the time of tool engagement (0-0.9 s), the phase where vibrations stabilize after the stabilization of the cutting process (0.9 to 9.0 s), and a phase with rapid drop in vibration levels in case of tool withdrawal. In order to reduce the effect of transients due to tool entry/withdrawal, the window from 4.60 s to 8.90 s was considered for the frequency domain analysis. As depicted in Fig. 8(b), the FFT spectrum obtained till the Nyquist frequency of 5000 Hz shows a broadband cluster of resonances ranging from about 4000 to 4300 Hz which appears to be related to machine–tool–toolholder structural resonances [47,48]. The analysis of the frequency band pertaining to machining presented in Fig. 8(c) reveals the existence of a prominent peak at around 105.6 Hz, showing that there exists an accumulation of vibration energy at a particular frequency related to the machining process. Other peaks of low amplitude have been identified around 14 Hz and 27 Hz and the expanded low frequency spectrum of Fig. 8(d) illustrates that there exists a harmonics relationship associated with the dynamic performance of the machine-tool and the low frequency vibrations of the structure [49,50]. In contrast to the highly dynamic unstable state represented by Experiment 25, there exist only low amplitudes and no dominant peaks with high amplitudes within the machining frequency range. The relatively low value of RMS of 14.246 indicates the stability of the cutting process and implies that the vibration amplitude level is tolerable for this optimum machining state [51,52].
FFT Analysis – Vx Radial for Experiment 25
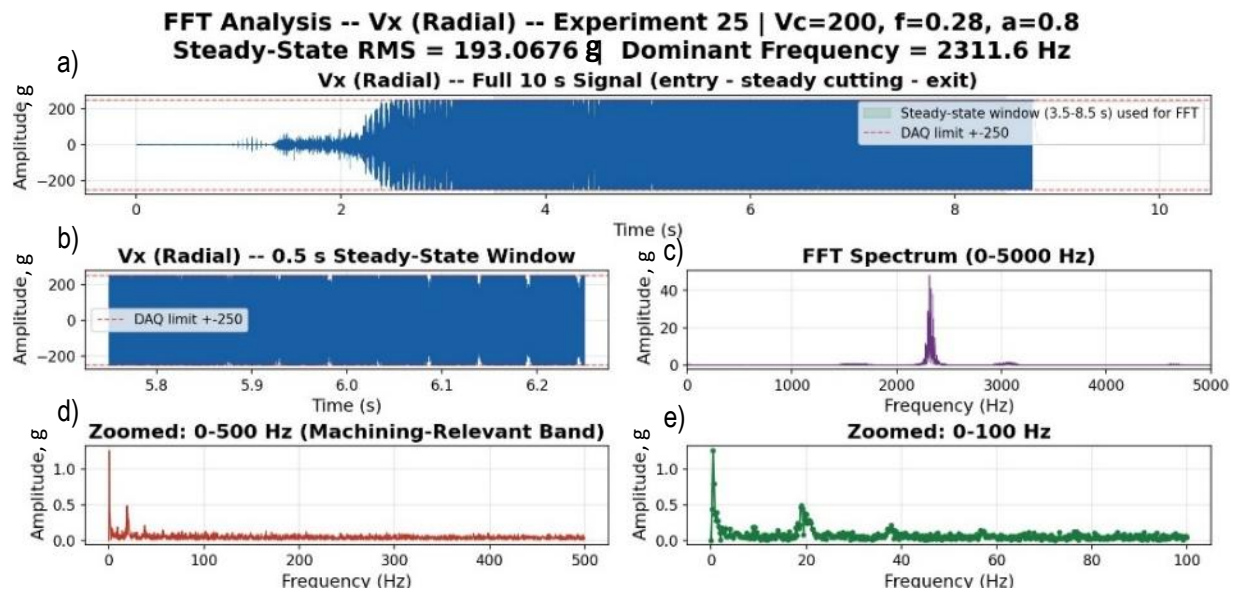
The FFT analysis of the signal of radial vibration (Vx) obtained from Experiment 25 (vc=200 m/min; vf = 0.28 mm/rev; ap = 0.8 mm) is illustrated in Fig. 9. As can be seen from Fig. 8(a), the signal in time domain has severe dynamic excitation and vibration amplitude reaches the data acquisition limits of ±250 mV during steady state cutting process. Furthermore, this is also indicated by the signal during steady state cutting process in Fig. 9(b) and extremely high value of RMS of 193.07 g. As indicated in the FFT spectrum presented in Fig. 9(c), there exists a high peak of the frequency at around 2311.6 Hz with several other nearby frequency peaks. Generally, the existence of a high peak at a particular high frequency is an indication of structural resonance induced dynamic instability in machining processes, especially where the excitation frequency is close to one of the natural frequencies of the machine-tool-workpiece system [47,48]. The machining-related frequency band depicted in Fig. 9(d) includes small-amplitude components alone, while the fine low-frequency spectrum of Fig. 9(e) shows a small peak close to 20 Hz, which could possibly represent the contribution due to spindle rotation and its harmonics. Such low-frequency components are very common during turning and are usually related to the contribution of spindle rotation, imbalance, or machine-tool dynamics instead of being induced by chatter vibrations [51]. This significant difference between low-frequency operational components and the strong peak of 2311.6 Hz implies that the vibration behavior is mainly determined by the high-frequency structural excitation [52].Therefore, the FFT analysis results clearly indicate the existence of dynamic instability during the above machining condition and explain the reason behind the large RMS vibration value, increased flank wear, and poor surface quality that result from these higher machining parameters. Some studies in the past have suggested that high vibration and chatter lead to high cutting dynamic forces, rapid tool wear, and poor surface topography [47-52].
Mechanistic relationship between tool wear, vibration (RMS) and surface roughness
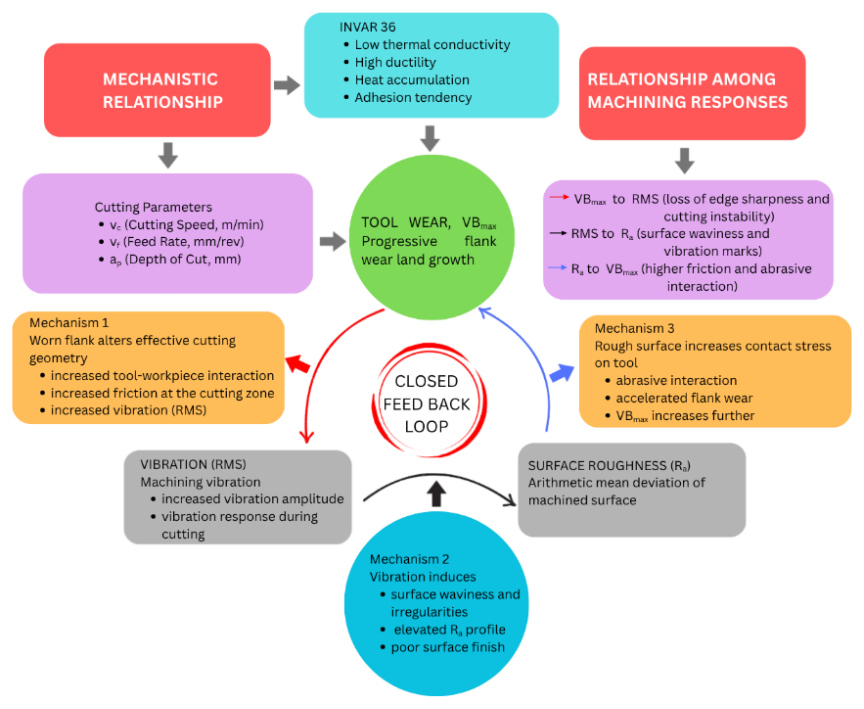
Figure 10 shows the closed feedback loop relationship among tool wear (VBmax), vibration (RMS) and surface roughness (Ra) in dry turning operation of Invar 36. The characteristics of Invar 36 such as low thermal conductivity, high ductility and adhesiveness result in increased heat generation in the cutting area, and hence the tool is prone to wear [43]. Besides, the chosen machining parameters such as cutting speed, feed rate and depth of cut affect the wear rate on the flank of the tool during machining. With the increasing flank wear, there will be a change in the cutting geometry which causes an increase in the friction at the tool-chip interface and at the tool-workpiece interface. The variation in cutting forces causes instability and increase in vibration amplitude, thus causing the rise in RMS values. Such relationship has been found in machining research for difficult-to-machine alloys [44-46,51]. This can be expressed using Mechanism 1, shown in Fig. 10. In Mechanism 2, there will be an increase in vibration produced during the process of cutting and transfer this vibration to the machined surface. Oscillations cause the formation of surface waviness, chatter marks, and geometrical deviations, thus increasing the arithmetic mean surface roughness. The vibrations of the tool and workpiece cause topography production, whereas there are other machining dynamics research showing the contribution of vibration instability to surface quality deterioration [47-52]. As the machined surface becomes rough, the cutting operation faces increasingly uneven contact conditions between the tool and the workpiece. The increased friction and abrasion thus lead to more flank wear formation and further damage to the cutting edge [43-46]. This wear mechanism is depicted in Fig. 10 by Mechanism 3. As a result, a positive feedback system will be generated where tool wear causes vibration, vibration leads to surface roughness, and surface roughness causes tool wear. From the above mechanical model, one can find the physical reason behind the results experimentally found in this study for the relationship between the VBmax, RMS vibrations, and surface roughness of Invar 36. The proposed feedback loop model helps to explain the relationship between VBmax, RMS vibration, and surface roughness from an experimental perspective. The study shows that tool wear, vibration formation, and surface damage occur at the same time through mutual physical phenomena, which is supported by earlier investigations reporting close relationships between tool wear, vibrations, dynamic stability, and surface integrity during machining processes [51,52].
CONCLUSIONS
Nickel-based alloys, especially INVAR 36, is a trending material in the research community. The present study explored the performance of the tool and alloy during the high-speed machining of this alloy. For the range of process input variables that are tested in the present study, the observations and conclusions can be drawn as follows –
The most significant parameter that affects both RMS vibration and VBmax is the cutting speed, while the feed rate has the maximum effect on Ra.
Optimum RMS vibration (14.246 g) and VBmax (0.110 mm) were achieved in Experiment 3 (vc = 150 m/min, vf = 0.18 mm/rev, ap = 1.2 mm), which means good machining stability and tool performance.
Surface roughness depends mainly on the feed rate, and the low values of the feed rate provide high surface finish since there will be no feed marks generated on the surface.
The optimum vibration frequency showed the concentration of energy vibration in the narrow band of low-frequency range, which is an indication of stable cutting and lack of dynamic instability.
Experiment 25 (vc = 200 m/min, vf = 0.28 mm/rev, ap = 0.8 mm) had the highest RMS vibration (193.07 g) and dominated the frequency at 2311.6 Hz.
The vibration and tool wear responses demonstrated almost identical behavior over the machining range under investigation, validating a high level of relationship between flank wear and vibration during dry machining of Invar 36.
Experiment 3 was found to be the best machining parameter by GRA, ARAS, and EDAS criteria, ensuring the effectiveness of the employed MCDM methods in the multi-criteria optimization of vibration, tool wear, and surface roughness.
Further research will be conducted in areas related to RSM-based predictive models, regression analysis, interaction effect investigation, formulation of energy-based machining model, and characterization of chatter via machine-tool dynamic stability analysis.

